Digital Traceability: The First 90 Days
Traceability projects rarely fail on technology. They fail because scanning is added on top of an existing workflow instead of replacing a step in it. Ninety days is enough to reach reliable roll-to-carton traceability if the sequence is right.
Days 1–30: map what already exists
Before buying anything, map every point where material identity is already recorded — fabric inspection reports, cutting tickets, bundle cards, packing lists. Most factories already capture 70 percent of the chain on paper. Digitising that chain is cheaper than inventing a new one.
- One PO, one style: trace it end to end by hand and time each handoff
- List every document that carries a roll, lot or bundle number
- Identify the two points where identity is currently lost
Days 31–60: label at the source
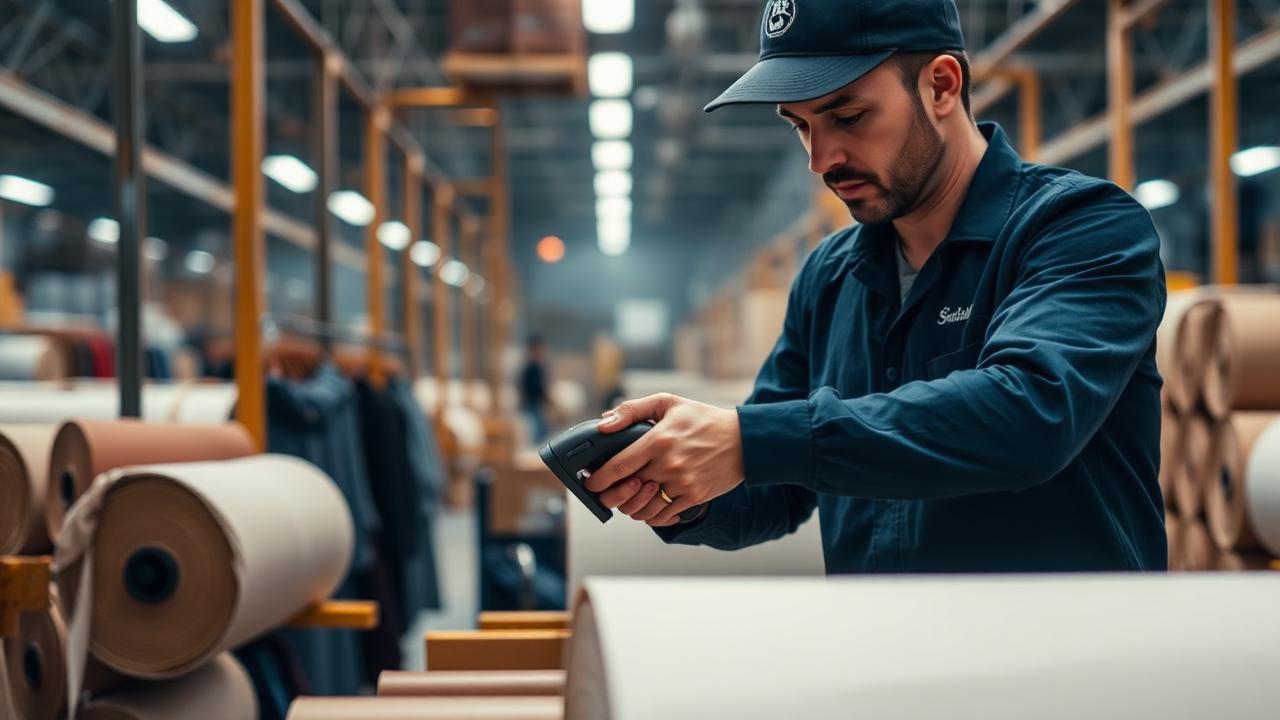
Traceability begins at goods receipt. Every roll gets a unique barcode tied to the supplier lot, shade band and test status at the moment it enters the store. If labelling starts later in the process, everything upstream stays invisible and the data set is permanently incomplete.
Keep the scan count low. Four scans — receipt, issue to cutting, bundle creation, carton packing — give the traceability most buyers ask for. Ten scans produce better theory and worse compliance.
Days 61–90: make the data load-bearing
Scanning survives only when someone downstream depends on it. Route a real decision through the data in the first quarter: shade-band segregation at cutting, or automatic hold on rolls without a passed test result. Once a supervisor cannot proceed without the scan, adoption stops being a training problem.
What to measure
Track scan completeness per stage, time from scan to record, and the percentage of cartons that can be resolved back to a fabric roll. A factory above 95 percent carton-to-roll resolution can answer almost any buyer traceability request within an hour.
More field notes
- AQL Sampling in Practice: Garment Quality Control Done Right
A practical garment quality control guide to AQL sample sizes, switching rules and the three habits that quietly invalidate a final random inspection.
- Lean Manufacturing Without Layoffs: Balanced Sewing Lines
Lean manufacturing in apparel: how line balancing, takt time and WIP control raise output while protecting operators — with the metrics that prove it.
- Chemical Compliance in Plain Language: RSL, MRSL and ZDHC
Textile chemical compliance explained for production teams — RSL, MRSL and ZDHC requirements, test evidence and a supplier checklist your factory can actually follow.