Lean Manufacturing Without Layoffs: Balanced Sewing Lines
Lean has a reputation problem on the sewing floor because it is often introduced as a headcount exercise. Done properly, line balancing removes waiting, not people — and the operators feel the difference first.
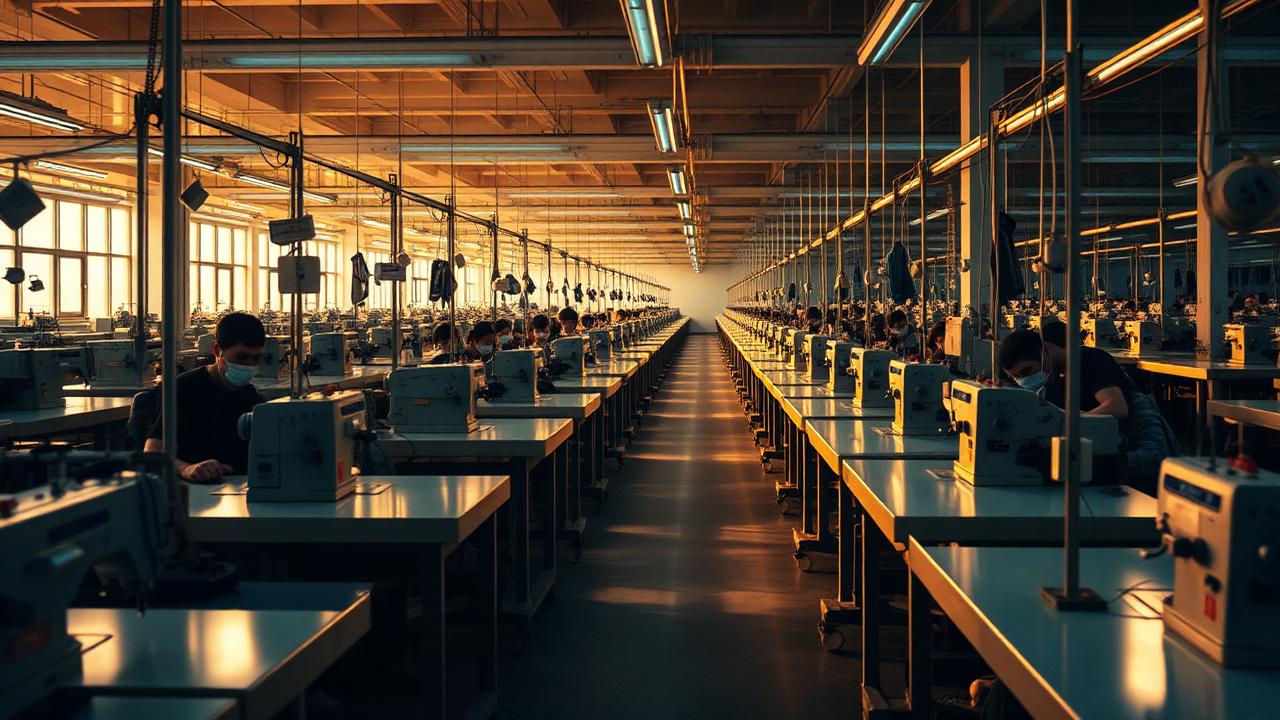
Balance against takt, not against the fastest operator
Takt time comes from the order and the working day, not from the best machine on the line. Once takt is fixed, every operation above it is a bottleneck and every operation far below it is an inventory generator. The goal is a flat operation-time profile, not a race.
Attack WIP before you attack minutes
Bundles queued between operations hide every problem in the line: a defect found three hours later cannot be traced to a cause. Cutting standard WIP from thirty bundles to six typically exposes two or three real bottlenecks in the first week and shortens defect feedback from hours to minutes.
- Set a visible WIP cap per operation and enforce it
- Move to smaller bundle sizes before rearranging machines
- Measure throughput time per garment, not only pieces per hour
Protect the operator in the design
A balanced line is also an ergonomic decision: reach distances, chair height, bin placement and lighting change achievable cycle times more than exhortation ever will. Improvements that make the work easier are the ones that survive the second month.
The metrics that prove it worked
Report line efficiency, throughput time, right-first-time percentage and absenteeism together. Efficiency alone can rise while quality and attendance fall — which is how lean programmes get a bad name.
More field notes
- AQL Sampling in Practice: Garment Quality Control Done Right
A practical garment quality control guide to AQL sample sizes, switching rules and the three habits that quietly invalidate a final random inspection.
- Digital Traceability: The First 90 Days
A realistic rollout sequence for material traceability, from PO mapping to shop-floor scanning discipline.
- Chemical Compliance in Plain Language: RSL, MRSL and ZDHC
Textile chemical compliance explained for production teams — RSL, MRSL and ZDHC requirements, test evidence and a supplier checklist your factory can actually follow.